A changeover procedure is the one document every shift swears it follows and no two shifts run the same way. The list says what to do. It rarely says in what order, and the order is where the minutes and the scrap hide.
Luis Clamps First. Marcus Sets the Rails First.
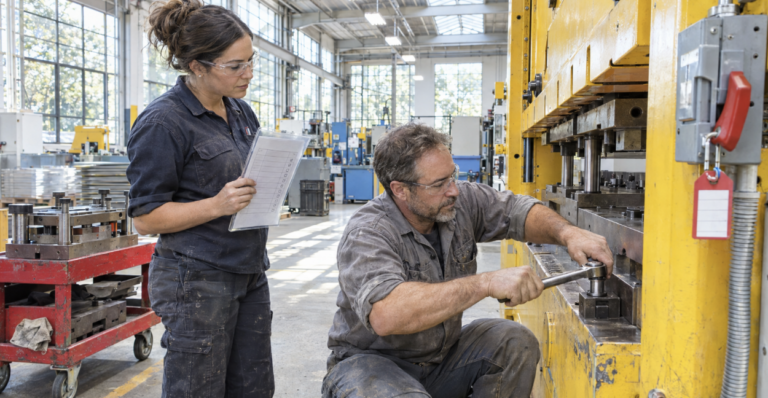
Luis and Marcus run the same press on different shifts, from the same one-page list. Luis clamps the die first and sets the feed rails second. Marcus does it the other way round.
Luis finishes in 38 minutes. Marcus needs 51. Second shift scraps the first parts after every changeover, and nobody has ever stood the two of them side by side. Both are following the sheet. The sheet just never decided between them.
Why Do Operators Run the Same Changeover Procedure Differently?
Because the list names the tasks and leaves the sequence to habit. Each operator builds a sequence that works for them, and then repeats it for years.
A 2014 Packaging Digest article on standard work describes exactly this. Operators who had a changeover procedures list still performed the tasks differently and “in varying orders.” The longer each one did it their own way, the greater the variation among operators. They seldom watched each other do it, so each assumed their way was the right one.
The article is a trade-press piece advancing a trademarked “ReducedEffort Principle,” not a controlled study, so I treat it as a pattern. It matches what I see on floors.
This Isn’t a Luis and Marcus Problem
It shows up in the data other people collect, too. A 2022 Food Engineering article by Vikram Mankar of GE Digital reports a food manufacturer whose data showed the same tasks taking different amounts of time depending on the operator shift. It also notes that missed changeover steps could cause setup errors and rejected product, and that new operators lacked the tribal knowledge of the originals.
Mankar works for a company that sells electronic work instructions, and the case figures come from unnamed manufacturers, so read it as a signal, not proof. Still, the two articles, eight years apart, describe the same gap. For the wider version of this problem, see our piece on operator-to-operator variation.
What the Market Sells Instead
In my view the market answers a different question. Quick-changeover programs ask how to make the steps faster. Digital checklists ask how to make sure the steps get ticked.
Both assume a sequence already exists and is agreed. At Luis and Marcus’s press it is not. A faster version of Marcus’s order is still Marcus’s order, and a tick box that records both orders as “done” records nothing about which one was right. Nobody had settled whose changeover procedure was the changeover procedure.
How Can We Standardize Work Across Shifts? Start With the Changeover
The changeover is the best place to start because it is short, it is frequent, and the two versions are visible side by side. Our guide to standardizing work across shifts covers the general method. The changeover just gives you a small, timed case to run it on.
The packaging article reports one case: at a major food manufacturer, one operator’s team lowered a 44-minute changeover to 22 minutes in four days. The article does not name the company, so treat it as an illustration. The article credits an effort-reduction method that cut tasks out of the changeover. It does not describe a side-by-side comparison, which is the step I add below.
Run the Side-by-Side Changeover Test This Week
You can do this without us. Here is the version I use.
- Pick the changeover with the most scrap or the longest downtime in the last month.
- Ask the most experienced operator on each shift to run it while you watch. Do not coach.
- On one sheet, write the step numbers down the side and the order each operator actually did them, with start and finish times.
- Mark three things: steps done in a different order, steps one operator did and the other skipped, and steps neither list mentions.
- Ask each operator why they do it that way. Write down the reasons in their words.
- Pick the sequence that gives the fewest rejects on the first parts, not the fastest one. Write it as a single numbered sequence.
- Have both operators run the new sequence once, then ask what got worse.
In my experience the second operator’s “extra” step is often the one that stops the first-part scrap. That is why you ask why before you choose. The same test works for the next changeover, and later it is how you update standard workwithout losing the standard.
How We Capture the Changeover Nobody Wrote Down
The test needs you on the floor for two shifts and a spare hour. Most plants never find it.
At SenseiLab we capture each operator’s real changeover, including the habits no sheet records. The supervisor puts the versions side by side and settles them into one validated procedure, which the operators then use at the press. When the way of working changes, the same capture runs again.
Frequently Asked Questions About the Changeover Procedure
What is a changeover procedure?
A changeover procedure is the written sequence for switching a machine or line from one product to the next. A useful one fixes the order of the steps, not only their names.
Why do operators perform changeovers differently?
Because a list of tasks does not fix the sequence, and each person settles into the order that works for them. The variation then grows the longer each person works their own way.
How can we standardize work across shifts?
Watch the most experienced operator on each shift do the same task, record the order and the time, ask why they do it that way, and agree on one sequence. Our article on how to standardize work across shifts gives the full method.
How do I standardize a changeover procedure?
Run the side-by-side test above, then write the winning sequence as one numbered list that both shifts have run once. Review it the next time the product, tooling or machine changes.
Book Your SOP Readiness Diagnostic
Luis and Marcus both think they are following the changeover procedure, and both are right. If you are not sure how many of your sequences differ between shifts, the free 30-minute SOP Readiness Diagnostic will show you where to look first, with no deck and no pitch.
Book the SOP Readiness Diagnostic: senseilab.io/book-a-call
About the author: Diego Echenique, MBA, is CEO & co-founder of SenseiLab, with 20+ years in manufacturing operations.