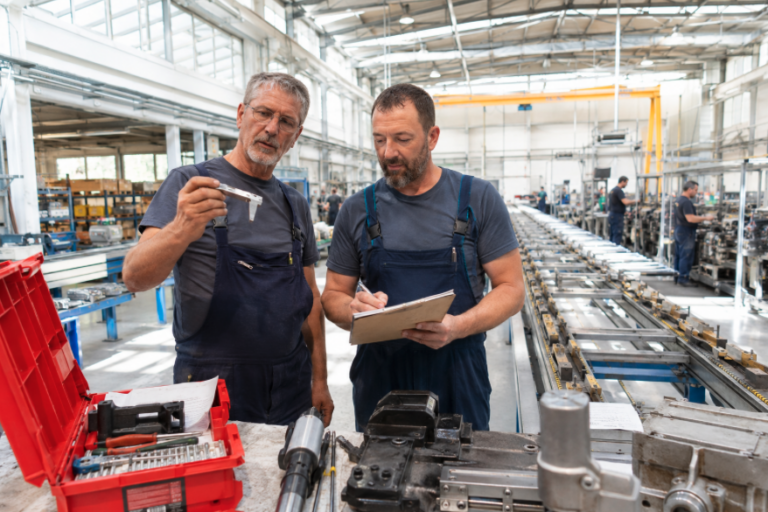
There were two men working at a bench near the end of the line, and neither of them appeared anywhere in the quality report.
No work order. No scrap ticket. No defect code. Just two experienced men quietly absorbing the distance between how the procedure reads and how the material actually behaves that week. They corrected parts all day. The line hit its number. The quality report showed nothing unusual, because nothing unusual had been recorded.
That bench is why anyone asking how to measure rework in manufacturing has to start somewhere other than the quality report.
Your rework number is not your rework number
Ask a plant manager what rework costs and you will get a percentage. It comes off a report. The report is built from tickets, and tickets get opened when something crosses a threshold that forces someone to stop, tag the part, and write it up.
Everything below that threshold is free, as far as the system is concerned.
It is not free. It is being paid in the most expensive currency the plant has: the attention of its most experienced people. And because nobody logs it, the payment repeats indefinitely.
The American Society for Quality’s long-standing benchmark puts the total cost of poor quality at somewhere between 15 and 20 percent of sales for a typical manufacturer. The part people skip past is ASQ’s second observation: the hidden costs of poor quality routinely exceed the visible ones by a factor of four. Most of what you are paying never appears as scrap at all. It shows up as slower throughput, missed dates, absorbed overtime, and two men at a bench.
When formal deviations do get written up, the individual price is not small either. PwC’s analysis of quality environments puts the industry average deviation cost between €22,000 and €48,000, and above €880,000 per deviation when product is lost. Those are the ones that got a ticket. The touch-up bench never opens a ticket.
Why the correction never becomes a procedure
Here is the part that turns a cost problem into a knowledge problem.
The correction those two men apply is not sloppiness. It is expertise. They know the mix runs short when the humidity climbs. They know which supplier’s batch needs the extra pass. They know the sound the press makes about four seconds before the part goes out of tolerance, and they know the window in which you can still pull it back.
That is high-value engineering judgment being applied in real time, for free, by people who were never asked to write it down and would not have known how to. It is tacit knowledge doing the job the document should be doing.
So the correction stays at the bench. It never reaches second shift. Second shift makes the same part badly tonight, and someone else corrects it tomorrow, and the loop runs forever because the loop was never visible.
This is the structural reason rework resists every fix aimed at it. Tighter process control assumes the process is understood and drifting. Better tooling assumes the tool is the constraint. A dashboard trends the scrap you already knew about. All three are aimed at the rework you can see. None of them touch the rework that is being silently prevented from becoming scrap by a person’s judgment.
And that judgment has a shelf life. Nearly 47 percent of manufacturers told the National Association of Manufacturers in its second-quarter 2026 outlook survey that attracting and retaining a quality workforce is a current business challenge. The bench does not survive the day those two men leave.
Run this in your plant this week: the four-column rework ledger
You do not need software for this, and you do not need us. You need one line, one week, and a clipboard.
Pick your most stable, best-understood production line. Not the problem line. The one everybody agrees is running fine. That is the point.
Ask the two most experienced people on it to keep a running log for five days. Four columns only:
- What I corrected. One line. Plain language, the way they’d say it to a colleague.
- Minutes. How long it took.
- Did I log it? Yes or no.
- Would a new hire have caught this? Yes or no.
Do not ask why. Why turns it into an investigation and people stop writing things down when it feels like an investigation. You only want what, how long, and whether the system knows.
At the end of the week, do three pieces of arithmetic:
The hidden multiplier. Total the minutes in column 2 where column 3 says “no.” Multiply by 50 weeks. Multiply by your fully loaded labor rate. Now put that number directly beside your reported rework cost on the same page. In most plants I have walked, the unlogged number is the larger of the two.
The exposure count. Count the rows where column 4 says “no.” Every one of those is a correction that exists only inside a specific person’s head. That is not a rework number. That is a risk register.
The propagation gap. Take the three most frequent entries in column 1 and go read the SOP for that step. Count how many of the three appear in the document in any form. The answer is usually zero, and that zero is the entire argument of this article.
Then extrapolate. If one well-behaved line produces that number in five days, multiply across your lines and ask what the honest annual figure is.
What actually closes the loop
The fix is not a better document. It is capturing the correction at the moment it happens, from the person making it, in their words, and turning it into a procedure that the next shift actually opens.
That is the work SenseiLab does. In a 30-day SOP Sprint we go on-site and operators, supervisors and engineers talk directly to our AI agent about how the job actually runs, including the corrections nobody ever wrote down. What comes out is five to ten validated Living SOPs that sit at the workstation and update as the process changes, plus one internal champion trained to keep extending the work after we leave. The ledger above is the five-minute version. The Sprint is the thirty-day version.
The bench is real. The correction is real. The invoice for both is already being paid, every week, out of a budget line nobody has ever seen.
Unless somebody counts it.
Book a free 30-minute SOP Readiness Diagnostic:
senseilab.io/book-a-call
FAQ
How do I measure the true cost of rework in manufacturing? Reported rework is only a fraction of the real figure. The American Society for Quality’s benchmark places total cost of poor quality at 15 to 20 percent of sales for a typical manufacturer, and notes that the hidden costs routinely exceed the visible ones by a factor of four. The rest is absorbed as slower throughput, overtime, and undocumented correction by experienced staff.
Why doesn’t rework show up in the quality report? Because reports are built from tickets, and tickets are only opened when a defect crosses a threshold that forces a stop. Corrections made below that threshold, in the flow of the shift, are never recorded, so they are structurally invisible to finance.
How do I measure hidden rework without buying software? Run a five-day, four-column ledger on one line: what was corrected, how many minutes it took, whether it was logged, and whether a new hire would have caught it. Total the unlogged minutes, multiply by 50 weeks and your loaded labor rate, and compare that number to your reported rework cost.
Why does the same rework keep repeating shift after shift? Because the correction lives in an experienced person’s judgment rather than in the procedure. It never propagates to the next shift, so the underlying condition is never actually fixed. The loop closes only when the correction is captured and written into a procedure people open.
Is rework a process problem or a knowledge problem? Both, but the knowledge side is the one nobody addresses. Process control, tooling and dashboards all target defects that already became visible. Undocumented correction is expertise preventing defects from becoming visible, which is why it survives every process-focused fix.